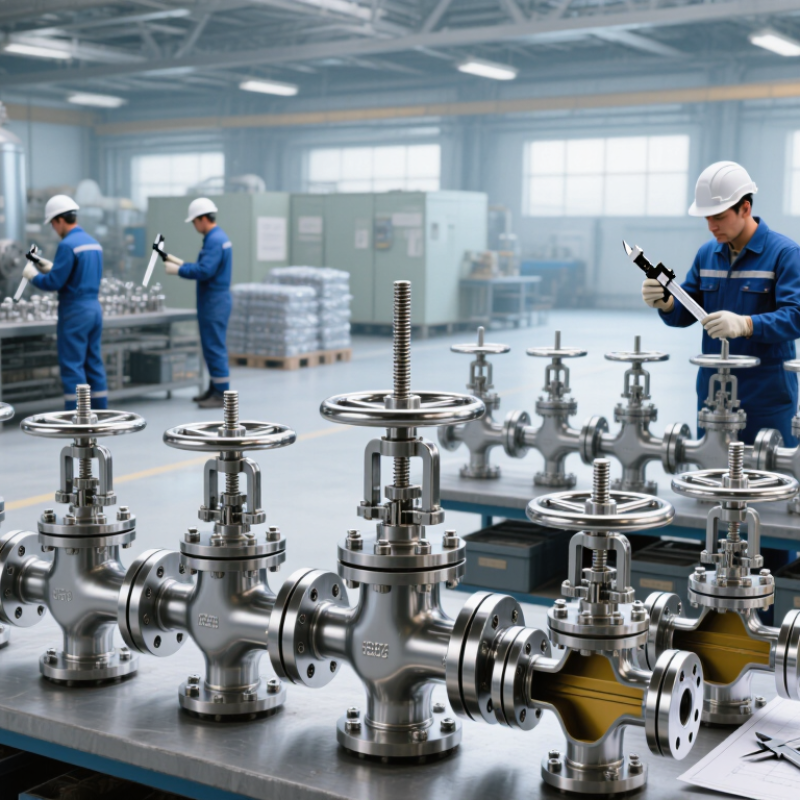
For global buyers, chrome-plated valve quality begins with the coating designation, not surface shine. ISO 1456 mainly covers electrodeposited nickel and chromium coatings on metallic components. It classifies coatings by service conditions, from mild indoor exposure to severe corrosive environments. The correct class depends on humidity, salt exposure, temperature, and handling.
A bright finish can still hide weak protection. Specify the nickel layer, chromium type, and minimum local thickness in the purchase document. Average thickness alone can mislead. Edges, threads, and valve corners often receive thinner deposits. Ask suppliers to identify critical measuring areas and inspection limits.
X-ray fluorescence supports fast, non-destructive checks. Cross-sectional examination can verify layered thickness when disputes arise. Sampling should include several valves, not only one attractive sample.
Buyers should also confirm whether the product uses decorative chromium or hard chromium. Not every hard-chrome valve coating falls within ISO 1456. This detail is easy to overlook. Salt-spray results can support evaluation, but they do not replace coating-thickness verification. A practical specification may require coating class, minimum local nickel thickness, chromium thickness, adhesion testing, and inspection records. Some purchasing sheets remain too vague. They should be revised after field feedback, because real corrosion often appears where drawings show nothing.